-
Before You Start: Know Your Meter and Your Environment
-
The 6-Step Checklist
-
Step 1: Check the Power Supply First
-
Step 2: Confirm the Output Type (Don't Assume PNP)
-
Step 3: Test the Output With the Fluke 87V (No Load)
-
Step 4: Repeat the Output Test With the Load Connected
-
Step 5: Check the Current With a Fluke 336 Clamp Meter
-
Step 6: The Overlooked Step—Wiggle the Cable and Connector
-
Step 1: Check the Power Supply First
-
Common Mistakes to Avoid
-
One Last Thing: Total Cost Beats Sticker Price
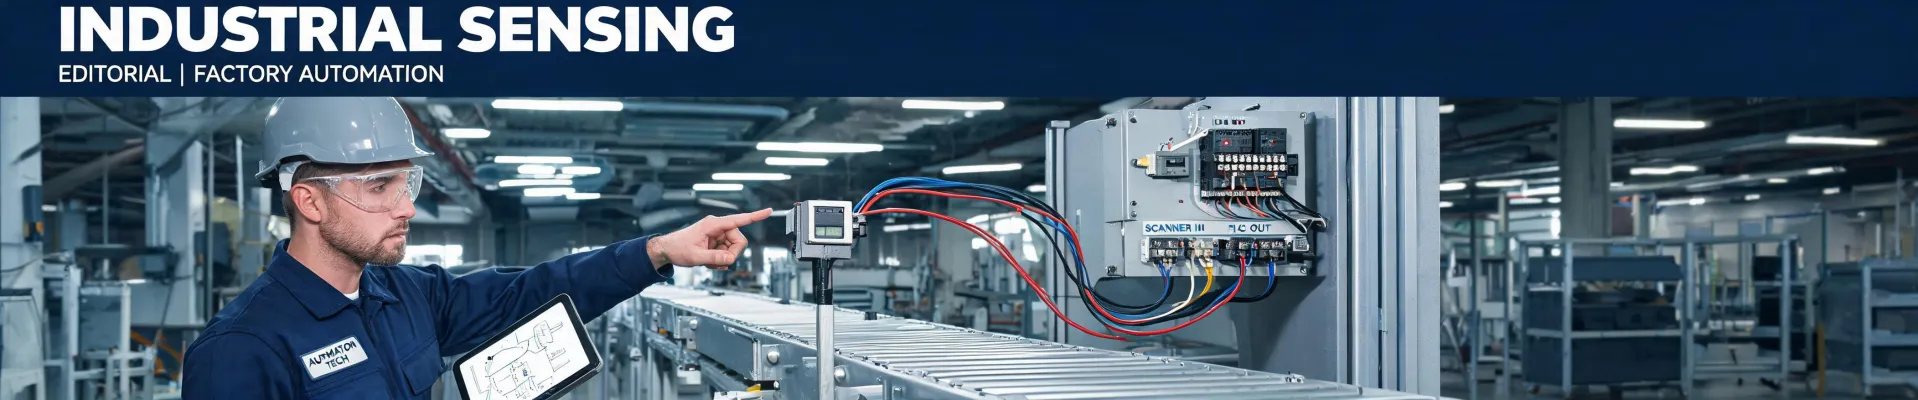
You're here because you want to know how to use a Fluke multimeter for sensor troubleshooting. Good. I've been an industrial maintenance tech for about 12 years, and I've personally made—and documented—14 significant troubleshooting mistakes, totaling roughly $18,700 in wasted labor and rushed parts. That's not a number I'm proud of. But it's why I keep a checklist, and why I'm writing this one down.
If you're dealing with a Turck proximity sensor that's acting up, or you just got asked to “check the sensors” on a line, this is the checklist I use. It assumes you've got a multimeter (we use the Fluke 87V true RMS multimeter in our plant) and a clamp meter for current checks (we use the Fluke 336 clamp meter). You don't need to be a controls engineer. You do need to go step by step.
What this is not: a full sensor theory lesson. This is the “try this in this order” list. Most sensor problems aren't the sensor—they're the wiring, the power supply, or the cable. This checklist is built around that.
Before You Start: Know Your Meter and Your Environment
First, safety. A proximity sensor usually runs on 24V DC. That's not normally lethal by itself, but industrial panels have other hazards. Use a meter rated for the environment. The Fluke 87V is CAT III rated. That matters more than people think. A cheap meter might read fine on the bench and then cause trouble when you're measuring near a variable frequency drive. I have seen it happen.
Choose a meter whose measurement category (CAT III, CAT IV) is at least as high as the circuit you are measuring. For plant floor control panels, CAT III is the usual minimum. Reference: IEC 61010-1.
Pull up the Turck proximity sensor catalog or the specific datasheet before you start. You need to know three things:
- Supply voltage range (usually 10–30V DC)
- Output type: PNP (source) or NPN (sink)
- Output function: normally open (NO) or normally closed (NC)
This was accurate as of early 2025. Turck's product line evolves, but those three specs don't change much for standard DC sensors.
The 6-Step Checklist
Step 1: Check the Power Supply First
I've lost count of the times someone swapped a sensor because the LED was off. Turns out the sensor was fine—the supply voltage was 14V instead of 24V. The PLC input might still pick it up, but a weak supply can cause no end of ghost faults.
Set your Fluke 87V to DC voltage. Connect black to COM and red to VΩ. Measure between the sensor's brown and blue wires (or pin 1 and pin 3 on an M12 connector). You should see something close to nominal supply. If it's below the sensor's minimum operating voltage, stop. Fix the supply first.
Why start here? Because a sensor can't switch if it's starving.
Step 2: Confirm the Output Type (Don't Assume PNP)
Any proximity sensor Turck ships will have the part number printed on the label. Read it. Most Turck DC sensors are PNP, but “most” is not “all.” NPN sensors are still around, especially in older machines. If you assume PNP and wire a PLC input accordingly, the sensor will test fine on the bench but do nothing in the machine.
Check the datasheet instead of guessing. I assumed “same specs” meant identical behavior across two similar part numbers—turned out one was PNP and one was NPN. That was a $900 mistake in emergency shipping plus a day of downtime.
Step 3: Test the Output With the Fluke 87V (No Load)
Now the actual sensor test. Most industrial proximity switches, including Turck's, are built to IEC 60947-5-2. That standard covers ratings and testing, but not troubleshooting, so think of the steps below as field practice. For a 3-wire DC sensor:
- Keep power connected.
- Set the meter to DC V.
- Black lead on blue (-), red lead on black (output wire).
- Present a metal target (or a piece of steel for an inductive sensor) to the sensing face.
For PNP NO: with no target, you should read about 0V. With target, the output should rise to near supply voltage, usually 22–24V. If the LED changes but the voltage doesn't, the output transistor is bad. That sensor is worth replacing.
For NPN NO: polarity reversed. With target, output should pull down near 0V. No target: it often stays near supply through a pull-up resistor, so the exact voltage depends on the circuit.
The 87V is a true RMS multimeter. That matters near VFDs and noisy machines, because an average-responding meter can read a distorted signal incorrectly.
Step 4: Repeat the Output Test With the Load Connected
Here's where a lot of techs stop too early. The no-load test tells you the sensor's output transistor can switch. It doesn't tell you it can drive the actual load—PLC input, relay coil, contactor. There's a difference.
Keep the meter on the same test points, but now let the sensor drive whatever it normally drives. The voltage should stay within about 2V of supply when the target is present. If it drops significantly—say, 24V down to 14V—you've got a connection problem or a load pulling more current than the sensor can source. A long, undersized extension cable can cause the same symptom.
People assume the sensor is bad because “it doesn't switch.” What they don't see is that the sensor is switching, but the voltage collapses under load.
Step 5: Check the Current With a Fluke 336 Clamp Meter
This is the step most people skip. A voltage reading tells you the sensor is switching. It doesn't tell you how much current is actually flowing. To check that, use a clamp meter without breaking the circuit.
Set the Fluke 336 clamp meter to amps DC (or AC, depending on your supply) and clamp around the output wire. Clamp around one wire only. Clamping around two wires cancels the magnetic field and you'll read zero. That's a classic rookie mistake. I've made it too.
What should you see? It depends on the load. A PLC input might only draw 5–10mA. A relay coil might draw 50–100mA. The point is to confirm current is actually there and reasonably close to what the datasheet says. If voltage looks right but current is near zero, look for a bad crimp, broken strand, or loose terminal.
Step 6: The Overlooked Step—Wiggle the Cable and Connector
Intermittent faults are the worst. The machine fails, the tech arrives, and everything works again. It's tempting to blame the sensor. More often, it's a flaky connection.
With power still on and your meter measuring output voltage, use something non-conductive—a plastic screwdriver handle or insulated pliers—to gently move the cable near the connector and along the run. Watch the meter. If the voltage blinks or drops when you wiggle, you've found an intermittent open. The sensor might be fine; the cable or connector is not.
I made this mistake in September 2022. I replaced a Turck proximity sensor after a “bad sensor” diagnosis. The next day, the same fault appeared. It turned out the M12 pigtail had a broken strand, and it only failed when machine vibration shifted it. That replacement cost $180 plus four hours of downtime. The fix was a $12 cable. I've caught 47 potential errors since then using this wiggle test. That's not an exaggeration; I keep a log.
Common Mistakes to Avoid
- Do not trust the LED alone. The LED can light even when the output can't drive the load.
- Don't test with a 9V battery if the sensor needs 10–30V. A voltage below minimum can create a false failure.
- Don't assume all dark-colored sensors are PNP. Read the part number and datasheet.
- Don't clamp around two wires with the 336. Clamp one conductor.
- Don't forget the mating cable. A damaged M12 cordset is incredibly common in washdown areas.
One Last Thing: Total Cost Beats Sticker Price
I've seen plants buy a no-name replacement sensor to save $50 and then lose a full shift when it failed. I'm not saying buy the most expensive option for every job. I'm saying consider the total cost: labor, downtime, emergency shipping, and the risk of a second failure. The cheapest replacement is rarely the cheapest fix.
That applies to test equipment too. The Fluke 87V and Fluke 336 cost more than a $30 meter from an online auction site. But when a false reading sends you down the wrong path for three hours, the “expensive” meter just paid for itself.
My experience is based on roughly 200 sensor failures in automotive assembly and packaging. If you're working in a different environment—say, food processing with high-pressure washdown—your checklist will include IP69K, chemical resistance, and steel-face considerations. I can't speak to every application, so use this as a starting point, not the final word.
Power, output, load, connection. In that order. That's the checklist.
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.
Leave a Reply