-
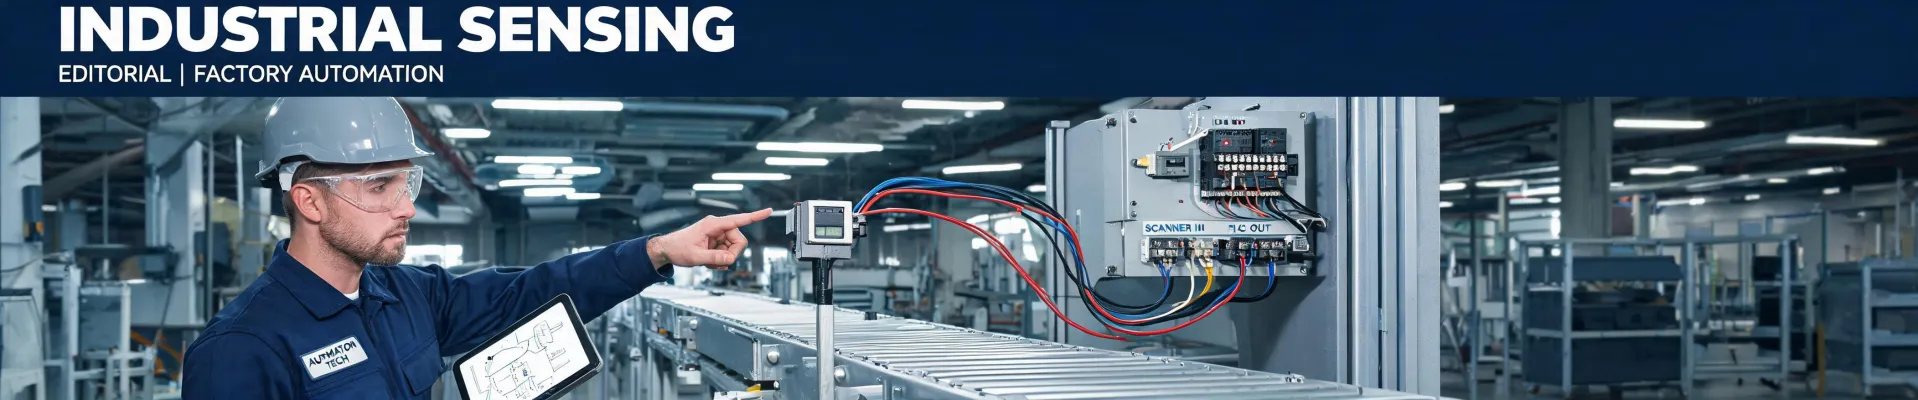
The most expensive decision I approved wasn't a Turck part
-
Capacitive sensing isn't inductive sensing with a different shape
-
When a sensor fails twice, let a data logger argue for you
- Measure brackets and shafts like the dimensions are real
-
'I don't have budget for the good part' — then make the temporary part visible
-
Bottom line: buy what you can measure and prove
I'm going to state an opinion that sometimes makes purchasing people uncomfortable: the most expensive sensor I ever bought was not a Turck sensor. It was the replacement that looked good on paper and cost me a weekend.
I've spent the last six years as procurement manager at a 43-person automation and machine-building company. I manage about $1.3 million in annual component and tooling spend, keep a cost tracker on every significant purchase, and I've signed for enough 2 a.m. replacement parts to know that unit price is only the opening bid.
Here's my stance: price per sensor is an input. Total cost per dependable year is the answer. And more often than not, that answer starts with Turck. You might think that's a sales pitch. It's not. It's what the cost tracker says after the failures, the re-orders and the downtime are all included.
Every time you buy a part by lowest price, you're also buying a probability. The invoice just doesn't show that probability.
I'd rather spend ten minutes explaining sensing technology to a project team than deal with mismatched expectations later. An informed team asks better questions and makes faster decisions. That's why I'm writing this out.
The most expensive decision I approved wasn't a Turck part
Last year I compared quotes for a sensor on a small indexing machine. The engineer specified a Turck uprox sensor. The other quote was $130 lower and looked identical: same thread, same housing, similar sensing range on paper. It looked like a no-brainer, so I approved it after making the engineer sign off on the substitution. That should have been the red flag.
Here's what we discovered: the cheaper sensor's sensing distance was specified on steel. The machine indexes aluminum blocks. A standard inductive sensor sees aluminum at a shorter distance than it sees steel, so the original mounting gap was wrong for the material. The sensor didn't fail exactly; it missed. Then it missed again. Someone adjusted the bracket, then someone added shims, then the machine missed a delivery window. The Turck uprox sensor, by comparison, has factor 1 characteristics. It detects all metals at the same rated sensing distance, according to Turck's technical documentation (turck.com; verify the current model). The cheap part cost me roughly $1,900 in labor and schedule by the time we stopped messing with it. The extra $130 I avoided? I spent about fifteen times that to learn the lesson.
Capacitive sensing isn't inductive sensing with a different shape
Another mistake that can show up in purchase orders is treating a Turck capacitive sensor as an inductive sensor for soft materials. It isn't. Capacitive sensors respond to changes in dielectric material, which makes them useful for detecting liquids through plastic or for checking whether material is present in a hopper or sight tube. A capacitive sensing task has its own sensing distance and calibration procedure.
If the target is metal in free space, an inductive sensor is often the answer. If the target is a non-metallic level or material-presence task, you need a capacitive sensor. A Turck capacitive sensor is a good starting point for those applications because it is designed for industrial conditions, but the key is choosing the right sensing principle before choosing the right part number.
This is why I keep the Turck sensor catalog in my office. When an engineer tells me what the material is and how far the target is, I can flip to the technology section instead of guessing. The catalog doesn't make the decision, but it prevents the back-and-forth that happens when someone orders by price first.
When a sensor fails twice, let a data logger argue for you
Here's the part of procurement that engineers sometimes find surprising: I love data loggers. In 2023, we started using a small data logger on a station that kept losing proximity sensors. The sensors were replaced, then replaced again, and the maintenance team was about to switch brands. I asked them to let me log supply voltage and temperature for one week before we spent more money.
The data logger showed the culprit. The 24 V supply was sagging below the sensor's minimum every time a large motor started. The PLC didn't reset, but the sensor electronics were not operating inside their published power range. The data logger caught it because it was there when the event happened. We fixed the power supply instead of replacing another sensor. The logger cost less than a service call and has paid for itself several times since.
If you don't know why something fails, you are not ready to buy the replacement. Log the environment first. That might sound like extra work, but it's cheaper than the wrong part, the re-order, and the second downtime event.
Measure brackets and shafts like the dimensions are real
The last line in my TCO spreadsheet is about measurement. A sensor bracket that is off by a few millimeters can ruin a sensing gap. A shaft that is the wrong size causes problems in the equipment the sensor is watching. I keep an outside micrometer set in the build area and another in maintenance. It's not only for inspection. It's for fitters who need to check a 20 mm shaft, a bracket thickness, or a spacer before they clamp it down.
How to use a Starrett micrometer, in five short steps
If you're going to buy an outside micrometer set, learn how to use it properly. Here's the short version I make every new hire practice:
- Clean the faces. A single speck of dust changes the reading.
- Close the spindle with the ratchet or friction thimble until it clicks two or three times.
- Check zero against the standard that comes with the set.
- Read the sleeve first, then the thimble scale. On a vernier model, read the extra digit if the tolerance needs it.
- Take a second measurement. If the numbers don't match, start over instead of forcing it.
That's the whole method. The tool is simple; the problem is people treating 'close enough' as a dimension. How to use a Starrett micrometer is not a secret. You close it gently, read it carefully, and let the ratchet tell you when to stop. The discipline matters.
'I don't have budget for the good part' — then make the temporary part visible
I hear this from my own engineering team, and I don't ignore it. I'm the person who closes the budget at the end of the year; I know what it feels like when the budget is red. If an application is temporary, or if a failure costs nothing but one hour of production, then the cheapest part that meets spec is legitimate. I still document the choice in the cost tracker, because I want to know if the temporary choice was actually temporary.
The false trade is saying that a solid part is a luxury. If the wrong sensor causes a spill, a crash, or a missed shipment, the initial savings disappears. A Turck uprox sensor is not expensive compared to one extra service call on a mixed-metal line. A Turck capacitive sensor is not expensive compared to one tank spill or one hopper overflow. An outside micrometer set is not expensive compared to re-machining a bracket because you guessed at the thickness.
Bottom line: buy what you can measure and prove
I'm not saying every project should have the most expensive component available. I'm saying the purchase decision should start with the physics and finish with the numbers: inductive sensing for metal targets; uprox if the metal type changes and the mounting distance needs to stay the same; capacitive sensing for non-metallic levels and material-presence tasks; a data logger recording the environment around any critical sensor or frequent failure; and a calibrated outside micrometer set on any bench where brackets, shafts, and gaps are set.
If someone asks me whether Turck parts are pricey, my answer is: compared to what? Compared to a missed deadline, a drained tank, or a 2 a.m. phone call, a sensor that does what its datasheet says is the cheapest option I know. That's not a slogan. It's what six years of procurement spreadsheets have taught me, and it's the only opinion that has survived contact with the production floor.
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.
Leave a Reply