The short version
The most expensive part in a sensor or lab-tool order isn't the hardware—it's the wrong setup. If your team can't find the correct Turck sensor wiring diagram, you'll pay for it in downtime. If they skip commissioning checks with a 373 clamp meter, you'll find the problem later. If they don't know how to use eppendorf repeater pipette correctly, reagent waste eats the discount. In my last audit, setup-related rework cost us $4,200—about 23% of the annual savings we thought we'd locked in.
That's not a guess. I'm a procurement manager at a 120-person industrial automation company. I've managed our MRO and instrumentation budget ($180,000 annually) for six years, negotiated with 40+ vendors, and documented every order in our cost tracking system. When I audited our 2023 spending, I found that the line item was rarely the problem. The problem was what happened after the box was opened.
Why I trust the datasheet more than the quote
Vendors compete on unit price because it's easy to compare. But total cost of ownership (TCO) doesn't sit in the quote. It sits in the wiring, the calibration, the training, and the rework. A Turck inductive proximity sensor M30 x 1.5 might cost $45 from one distributor and $52 from another. That $7 difference is noise if the wrong output type (PNP vs. NPN) stops a line for two hours.
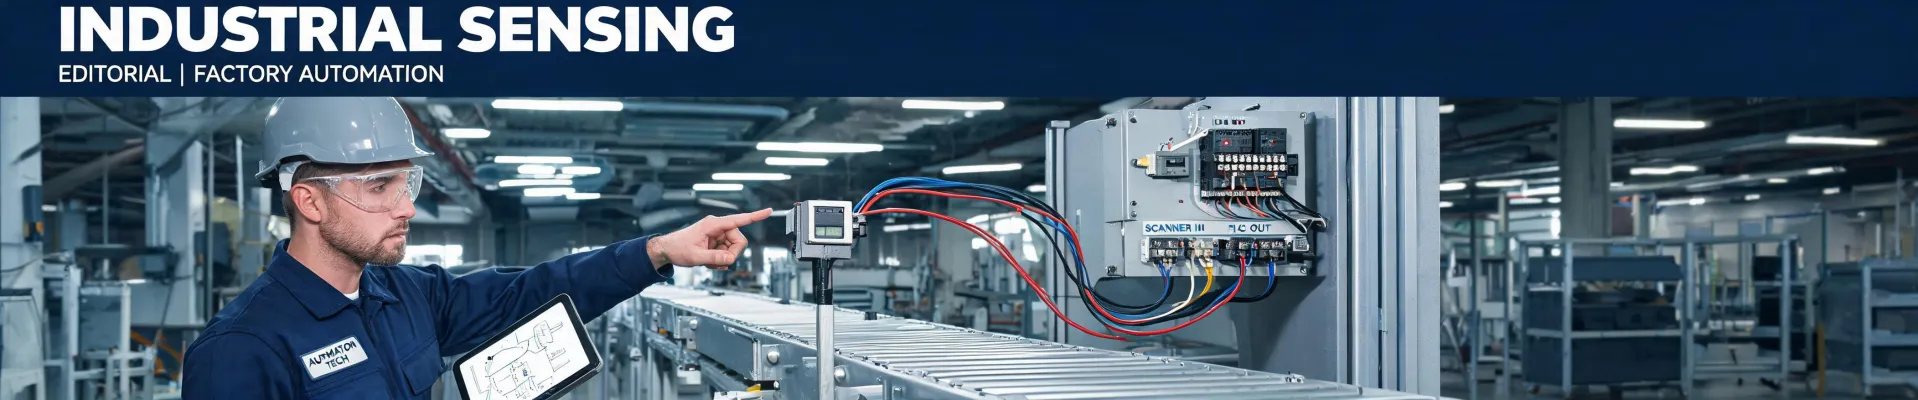
So our policy now requires the official product datasheet and a current Turck sensor wiring diagram before we approve any new sensor purchase. Not a forum photo. Not a generic drawing from an old project folder. The exact model page. Turck's online catalog and datasheets (accessed January 2025) are the authority. Pinouts can change by connector type, cable length, and sensor family.
What this looks like in practice
Turck inductive proximity sensor M30 x 1.5
The M30 x 1.5 thread is common, but 'common' isn't 'universal.' You need to confirm sensing distance, flush or non-flush mounting, shielded or unshielded, and output logic. A Turck inductive proximity sensor M30 x 1.5 with the right specs can last years. The same sensor with the wrong wiring can fail in a week—or worse, damage an input card.
IEC 60947-5-2 covers proximity switches, but it won't tell you which wire is which on your connector. The Turck datasheet will.
I knew I should verify the wiring diagram against the actual sensor label, but thought 'what are the odds they changed the pinout?' That was the one time it mattered. The electrician reused a cable from a different Turck model. Two wires were swapped. We caught it after a $1,200 redo and six hours of lost production. Now the rule is simple: no wiring diagram, no install.
The checklist: exact model number, official wiring diagram, connector pinout, and a confirmed sensor output. In that order.
Photoelectric sensor
A photoelectric sensor is a different animal. Diffuse, retroreflective, through-beam—they all solve different problems. Buying a cheaper diffuse sensor when you actually need background suppression will create false triggers every time a shiny part passes. Dust, coolant mist, and ambient light will make a bad choice look intermittent.
The most frustrating part of sensor selection: the same failure looks like a maintenance issue, not a procurement issue. You'd think a model number would prevent misunderstanding, but sensing mode, range, and response time get lost between the line engineer and the PO. What finally helped was a one-page spec sheet signed by both maintenance and engineering before purchase.
For photoelectric sensors, I ask three questions: What is the target? What is the background? What is the environment? If the vendor can't answer against the datasheet, the price doesn't matter.
373 clamp meter
We also use a 373 clamp meter during commissioning. It's not a sensor tester. It's a reality check for current draw on motors, heaters, and pumps. A sensor might tell you a valve is open, but the clamp meter tells you whether the pump is actually running within expected current.
So glad I double-checked a new conveyor circuit last Q2. Almost signed off because the sensor LEDs looked correct. The 373 clamp meter showed an imbalance on one leg. Turned out a terminal wasn't torqued. That would have burned a motor contactor within a month. The meter didn't cost us anything that day; skipping it would have cost plenty.
Eppendorf repeater pipette
On our lab side, the same TCO logic applies. An Eppendorf repeater pipette is a precision tool, not a plastic dispenser. If you want to know how to use eppendorf repeater pipette correctly, the answer isn't in a quick YouTube short. Prime the tip, check the seal, keep a consistent angle, and avoid overfilling. Small errors in repetitive dispensing multiply across a 96-well plate.
We bought two repeaters last year. The unit price was visible. The reagent waste was not. After a 20-minute training session with the lab lead, our tip-misfit complaints dropped from about one per week to one per month. That saved a $700 reagent lot in the first quarter. Not huge, but real.
Where this advice doesn't apply
I'm not saying every purchase needs a committee. If you've used the same Turck M12 connector for five years and buy from an authorized distributor, price shopping is fine. The datasheet-first rule matters most when you're specifying a new sensor, changing vendors, or mixing old and new hardware.
I've never fully understood why some vendors make pinout variations so hard to find. My best guess is legacy product lines and regional versions. If someone has insight, I'd love to hear it. I should add that we're not an OEM; our volumes are modest. A high-volume manufacturer might negotiate different terms.
Also, I'm not an electrician or a lab compliance officer. Verify all wiring with qualified personnel and local codes. Calibrate pipettes on schedule. Use the manufacturer's current instructions for any safety-critical device.
But for our shop, the pattern holds: the datasheet is the discount. The wiring diagram, the spec sheet, the commissioning check, and the training are what keep the total cost down. The unit price is just the entry fee.
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.
Leave a Reply