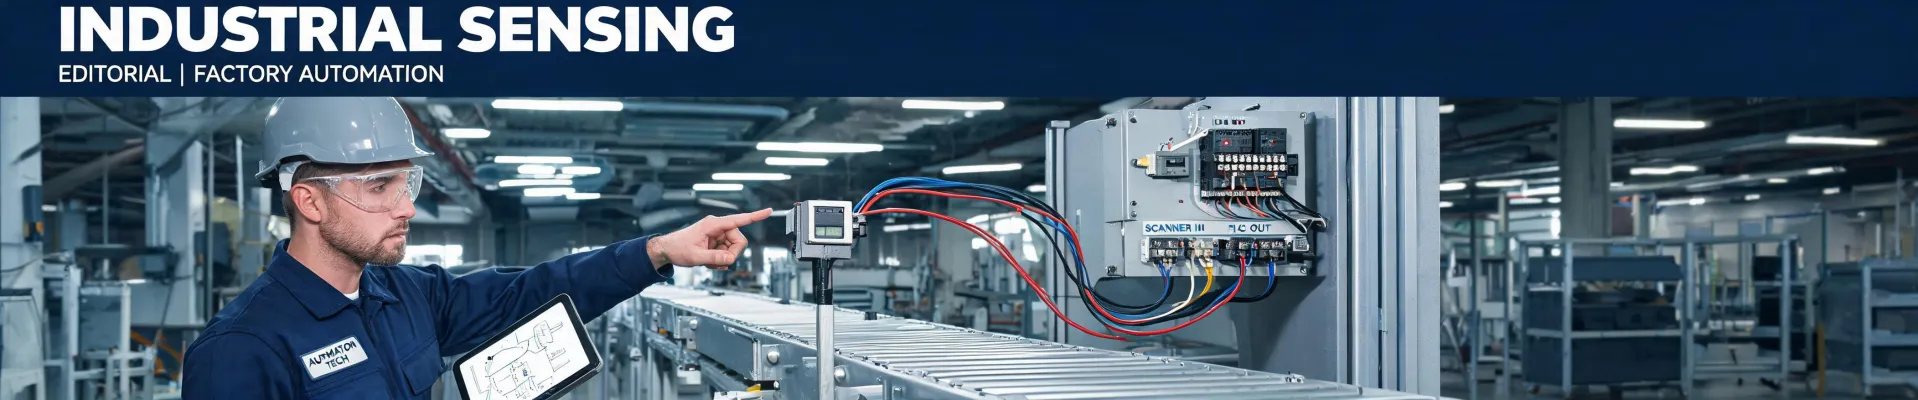
It's 2:17 AM at a packaging plant. A case erector has stopped mid-cycle. The fault code points to a proximity sensor. A technician grabs a spare Turck proximity sensor from the crib, swaps it in, cycles the machine, and it runs. For 40 minutes. Then the same fault returns.
I've been the person on the phone during calls like that. I coordinate emergency maintenance and rush parts for an industrial automation integrator. I've handled 300+ rush service calls over 12 years, including same-day turnarounds for automotive, food, and packaging clients. And I'll say this plainly: most of the time, the Turck proximity sensor wasn't the root cause. The replacement just reset the symptom long enough for the line to start again.
The surface problem: we replaced the sensor, so why is it still failing?
When a machine faults on a proximity sensor, the fastest move is to swap it. That's not lazy. It's triage. If the spare fixes the fault for a shift, everyone moves on. But if the same fault comes back, you don't have a sensor problem anymore. You have a sensing system problem that keeps punishing the sensor.
This is the part that gets missed in emergency maintenance: a replacement part can be technically correct and still fail because the conditions around it are wrong.
The deeper reason: a proximity sensor is only one link in the chain
People treat an inductive proximity sensor like a light bulb. It works or it doesn't. But an inductive sensor is part of a chain: target material, sensing distance, mounting, connector, cable, input card, power quality, and the machine's mechanical repeatability. If any link is marginal, the sensor gets blamed because it's the easiest part to swap.
Target material and sensing distance
Inductive sensors respond to metal, but not all metals equally. A standard inductive sensor rated for 8 mm on mild steel may only see 4-5 mm on aluminum or stainless. If someone grabbed a same-size replacement without checking the Turck catalog for the correct correction factor, the sensor may work when the machine is cold and fail when it warms up.
Some Turck uprox sensors offer extended sensing ranges and better performance on non-ferrous targets, but they're not a substitute for checking the datasheet. This is where a 24 digital caliper earns its keep. Don't guess the air gap. Measure it. Measure the target thickness. Measure the mounting depth. I've seen a 0.5 mm difference turn a stable signal into an intermittent one. A caliper won't tell you the correction factor, but it gives you the real numbers to compare against the datasheet.
Electrical noise and grounding
In one March 2024 call, a client had replaced the same Turck proximity sensor three times in two weeks. The sensor tested fine on the bench. On the machine, it dropped out whenever a nearby VFD ramped up. The issue wasn't the sensor. It was a damaged shield connection and a missing ground bond.
This is where a Fluke 376 FC clamp meter and an Extech multimeter become diagnostic tools, not just electrical toys. The 376 FC clamp meter is useful for checking current without breaking the circuit, and for spotting unexpected leakage or shared neutrals. If you're wondering how to use Extech multimeter for sensor circuits, start simple: verify 24 VDC at the sensor, check the switching output against the datasheet, and confirm the input card sees the same state. Then check ground continuity. A lot of intermittent sensor faults are actually noise problems wearing a sensor costume.
Mechanical mounting and connector problems
I have mixed feelings about quick-disconnect connectors. On one hand, they make replacement fast. On the other, they can hide a bent pin, a loose coupling, or moisture ingress until the machine is running at full speed. I went back and forth between blaming the sensor and blaming the cable for two days on a food plant job. Ultimately, the problem was a connector that wasn't fully seated after a washdown. The sensor was fine. The connector wasn't.
So glad I checked the coupling before we ordered another emergency sensor. We were one purchase order away from paying overnight freight for a part we already had on the shelf.
The spare part wasn't actually equivalent
This one hurts because it looks so responsible. A tech grabs a spare that fits mechanically. The thread is the same. The connector is the same. But the output type, sensing distance, shielded vs. unshielded, or temperature rating is different. It works for now. It fails later. And because it's a Turck proximity sensor, everyone assumes Turck is the problem.
That's why I keep a current Turck catalog bookmarked and a PDF copy on my phone. Not because I love reading catalogs, but because part numbers encode more information than the housing shows. If you're searching for a proximity sensor Turck replacement, match the full part number or the exact datasheet characteristics. Don't match by appearance.
What this costs you
The obvious cost is downtime. A packaging line can lose thousands of dollars per hour. But the hidden cost is worse: repeated emergency orders, expedited freight, and the credibility hit when maintenance says fixed and the line stops again two hours later.
I have seen a plant pay $800 in rush freight for a sensor that cost $120, only to discover the real fault was a loose ground. I have also watched a maintenance team lose the production manager's trust because they kept swapping parts instead of diagnosing the system. That trust is harder to rebuild than any sensor inventory.
According to IEC 60947-5-2, inductive proximity sensors have defined sensing distances and operating conditions. The standard doesn't cover your mounting bracket, your cable routing, or your maintenance habits. Those are on you. And they are usually where the failure lives.
What actually works: a short commissioning checklist
I'm not going to pretend this is complicated. The fix is boring. That's the point.
- Match the exact part. Use the Turck catalog to confirm sensing distance, output, housing, connector, and temperature range. If the part number changed, check the cross-reference. Don't assume.
- Measure the mechanics. Use a 24 digital caliper to verify air gap, target thickness, and mounting depth against the datasheet. Check for metal chips, weld slag, or loose brackets.
- Verify the electrical path. Use the Fluke 376 FC clamp meter for current checks and an Extech multimeter for voltage and output state. If you're unsure how to use Extech multimeter in a noisy panel, keep the leads short, use the min/max function, and compare the sensor output to the PLC input.
- Inspect the connector and cable. Disconnect, inspect pins, check strain relief, and confirm the coupling is seated. On washdown machines, look for moisture inside the connector.
- Test under real conditions. Run the machine through its full cycle, not just a jog. Watch the sensor LED or PLC input during the exact moment the fault used to occur.
- Keep critical spares. Not every part number. Just the ones that stop the line. Label them. Check them. Rotate them.
The real fix is a diagnostic habit
I'm still not sure why some technicians jump straight to replacement while others reach for a meter first. My best guess is that replacement feels faster in the moment. It's visible. It's decisive. But it doesn't scale, and it doesn't build trust.
Quality of maintenance is a brand signal. When production sees a tech show up with a Turck catalog, a caliper, and a clamp meter, they don't just see a repair. They see a team that treats uptime as a process, not a guess. The sensor is just one part. The diagnosis is the product.
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.
Leave a Reply